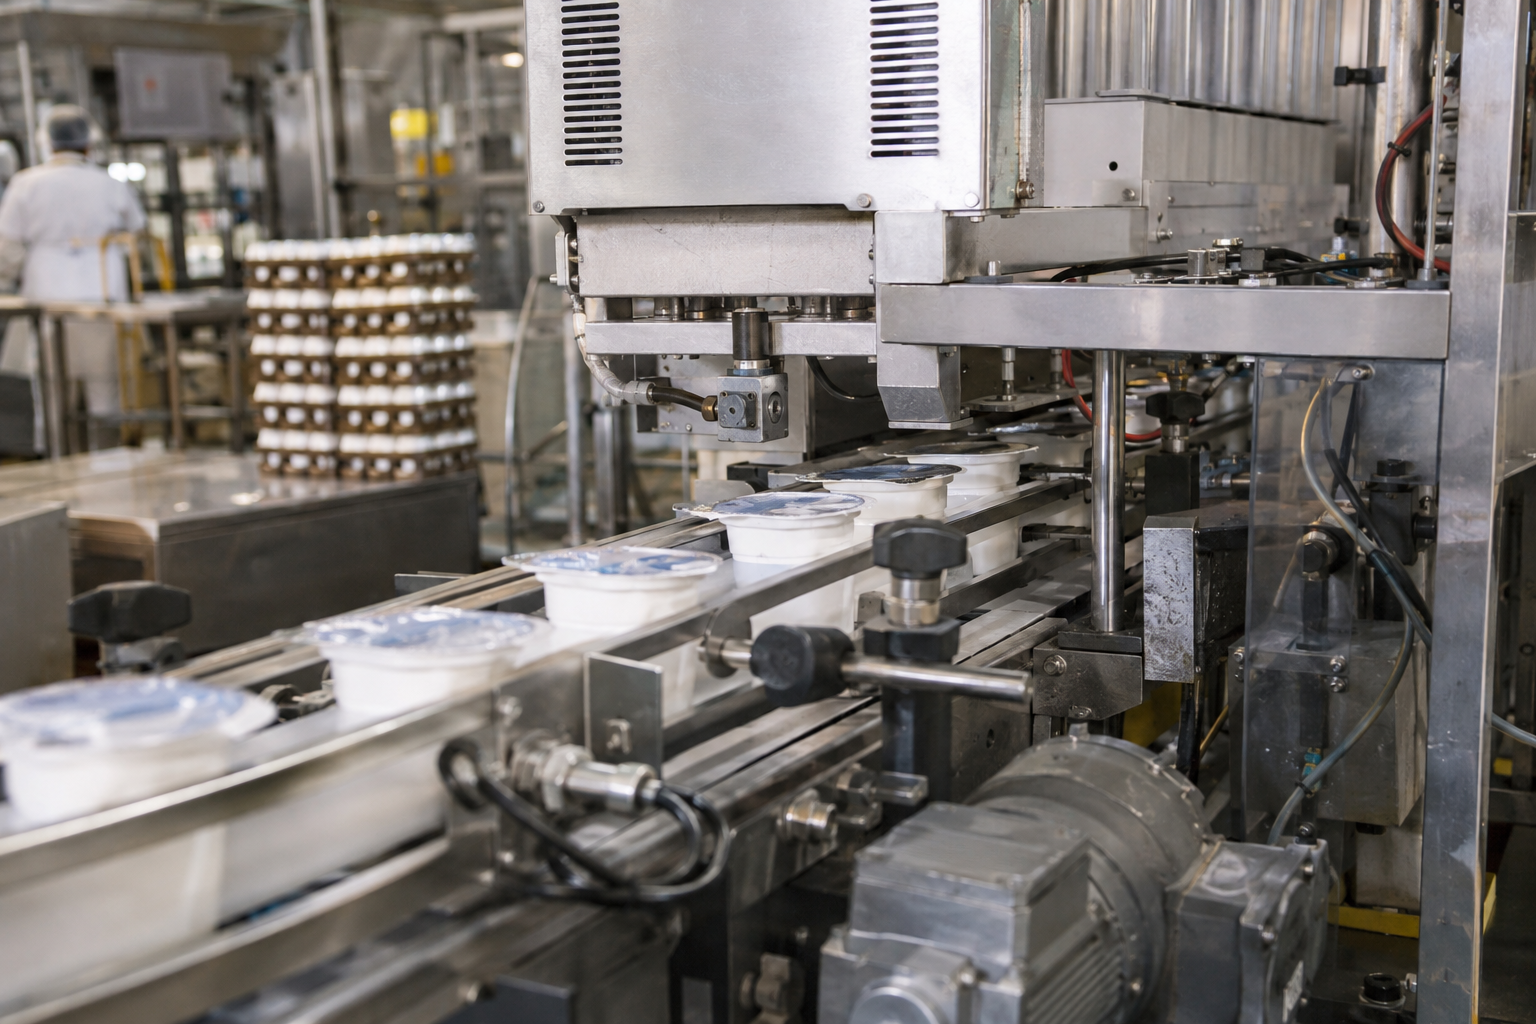
When the Product Changes Faster Than the Filler Settings
The first challenge is often product variation, not machine capacity. A dairy product may behave differently after a temperature change or an extended hold. Foods containing particulates can settle, bridge or distribute unevenly. If the equipment trial uses only one convenient batch, the plant may approve a filling process that works within a much narrower window than production requires.
Compare filling approaches against the actual product characteristics. A flow-based system, piston filler or weighing arrangement may each offer advantages, but suitability depends on viscosity, air content, particulates, accuracy requirements and cleanability. Upstream agitation or temperature control might stabilize filling, although either can affect product quality and add operating complexity.
Trial representative products at the boundaries of the approved process window. Check fill consistency after startup, a brief stop and a longer interruption. Observe foaming, dripping, splashing and particulate handling, not just the reported average fill. Agree beforehand how samples will be taken and evaluated. A stable average can hide individual packages that need investigation.
A Good Seal Must Survive More Than the Sealing Station
Seal failures often begin before the package reaches the sealing head. Product on a flange, condensation, container distortion or inconsistent presentation can undermine an otherwise suitable sealing process. Increasing heat or pressure may appear to help, while creating new problems with package deformation, opening performance or material damage.
Compare correcting the contamination source with changing the sealing arrangement or packaging material. Better nozzle cutoff and container control may address the cause without introducing another material specification. A different closure system may be justified, but it brings purchasing, tooling and validation consequences.
Use production-intent containers and closures in the trial, including representative material variation. Examine seals after the handling, cooling and storage conditions the package will actually encounter. Have quality personnel define appropriate integrity and opening tests before the run. Visual appearance alone should not determine acceptance, and a packaging trial does not replace any required food safety or shelf-life validation.
Cleaning Access Can Decide Whether the Layout Works
A compact installation becomes a liability when sanitation staff cannot reach a product-contact part or inspect a concealed surface. Floor space matters, but fitting equipment into the available footprint is not the same as making it maintainable. Guards, utilities, drains and adjacent conveyors all affect access.
Evaluate manual cleaning, clean-out-of-place tasks and any proposed clean-in-place functions separately. A machine may use more than one method. Automated cleaning can reduce repetitive handling, but it still requires a suitable process and verification. Removable assemblies offer access, yet introduce lifting, storage and reassembly tasks.
During a trial or equipment review, ask the people who will clean the system to demonstrate the proposed sequence. Time the complete activity, including safe isolation, disassembly, inspection and reassembly, rather than only the wash portion. Review chemical and temperature compatibility, drainage, allergen changeover requirements and opportunities for contamination during maintenance. Reserve working space on the layout before installation details become difficult to change.
More Filling Capacity Can Simply Move the Queue
A faster filling operation does little for output when containers repeatedly stop at labeling, inspection or case packing. Short downstream interruptions can also create excessive product dwell time or unstable restarts. The useful question is how the complete line recovers, not how quickly one machine runs without interruptions.
Accumulation can absorb some stops, but it consumes space and can expose delicate packages to pressure or unnecessary handling. Better controls coordination or a downstream equipment change may be the stronger choice. Map the expected stop conditions and decide where packages can safely wait.
Challenge the integrated sequence deliberately. Simulate a downstream stop, container shortage, reject event and restart. Confirm that product delivery responds appropriately, rejected packages remain controlled and operators can identify the original fault. Where full integration cannot be demonstrated before shipment, document which checks must be completed at the plant and who owns them.
Flexibility Only Counts When the Next Shift Can Repeat It
Frequent format changes expose weaknesses that a single-product demonstration misses. Adjustable equipment can serve a wider package range, but additional settings create more opportunities for inconsistent setup. Dedicated change parts may simplify positioning while adding storage and identification requirements.
Trial a representative changeover with plant operators, then check the first acceptable packages and the stability of the following run. Record tools, settings, inspections and training needs. Turn unresolved issues into acceptance criteria rather than informal promises. To begin that application review, visit the Pure Packaging Solutions [Food and Dairy Packaging page](/industries#food-dairy), with the option to request a quote based on your products, packages and operating constraints.