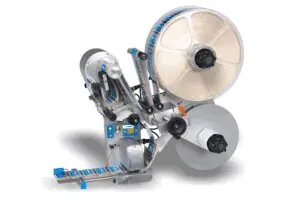
Should we print directly on the package or apply a label?
Start with the information requirement, not the print technology. A short date or lot code may suit direct printing, while extensive variable text, graphics or logistics information may favor a printed label. Separate fixed artwork from information that changes by product, batch or package. Then identify who must read it, where it must appear and whether it needs machine verification.
The deciding dependency is the package surface throughout its handling cycle. A mark that looks acceptable immediately after application may smear during conveying or lose contrast after refrigeration. A label may lift at a seam or on a damp container. Test actual production materials through filling, cooling, packing and representative storage. For Canadian distribution, include applicable language requirements in the artwork review rather than discovering that the available print area is inadequate after equipment selection.
Where should the applicator or coder sit on our line?
Place it where the package is controlled, the target surface is accessible and operators can service the equipment safely. Stable presentation usually matters more than finding an empty conveyor section. Review container spacing, rotation, vibration and transfers. Flexible packs may need backing support; round containers may need controlled orientation. Keep printheads and dispensing components accessible without making routine adjustments require a prolonged teardown.
The main dependency is package behavior at the proposed location. Filled containers can travel differently from empty ones, and accumulation can change spacing unexpectedly. Observe normal running, restarts and downstream stops before fixing the layout. Include room for inspection and reject handling where required. A coder squeezed into a convenient gap can create persistent tracking problems if packages slip or rotate between the trigger sensor and the marking point.
How do we keep the right code tied to the right product?
Treat message selection as part of the production recipe. Define where product names, lot identifiers, dates and barcode data originate, who can edit them and how they are approved. Use controlled templates rather than asking operators to rebuild messages at each changeover. Establish what happens when a recipe is missing, a connection fails or an operator selects a product that does not match the scheduled order.
The caveat is that automation cannot correct an incorrect source record. Assign ownership of master data and date calculation rules before connecting the coder to a plant system. During commissioning, challenge the setup with wrong recipes, unavailable data and interrupted communications. Confirm that the line responds as intended and does not silently continue printing the previous job.
Do we need a camera, a barcode reader or a reject system?
Choose inspection according to the failure you need to detect. Presence detection can confirm that a label exists, but not that its content is correct. A barcode reader can check encoded data; character inspection can assess printed text against an expected value. A successful barcode read alone does not establish conformance to a specified barcode quality standard. Write separate acceptance criteria for each requirement.
Inspection effectiveness depends on package tracking and the response to a failed check. Define how the failed package reaches the reject point, how removal is confirmed and what happens if rejection fails. Test these sequences, not just image quality. For pharmaceutical applications, align inspection, access controls and records with the site's quality and validation requirements.
What should we standardize to make changeovers less troublesome?
Standardize repeatable setup references: package guides, applicator position, sensor location, approved messages and consumable identification. Record settings in the format operators actually use. Include cleaning access, consumable loading and a first-package approval step in the changeover procedure.
The dependency is format variation. A setting that works for one bottle or carton may not transfer reliably to another. Prove each format and record exceptions instead of forcing every package into one setup.
What should we bring to an equipment evaluation?
Bring representative packages, approved artwork, variable data examples, line layouts and the intended operating conditions. Define pass and fail criteria before trials, covering placement, readability, adhesion or mark durability, changeover tasks and fault recovery. Ask to see stops, restarts and replenishment, not only uninterrupted operation.
Trial conclusions depend on how closely the samples and conditions represent production. Record anything the test cannot reproduce and plan an on-site acceptance check for those gaps. To discuss the application with Pure Packaging Solutions, visit the [Labeling and Coding page](/solutions#labeling-coding), where you can also request a quote. Include the package range and acceptance criteria so the discussion starts with engineering requirements.